“I Meant to Do That”
First up, an important message from former KISPer TC. He sent out an email requesting prayer for a fallen soldier:
Mark’s a good friend. He’s in Landstuhl Army Hospital after being shot in the head in Afghanistan.
Two other Georgia Guardsmen were killed on Monday, bringing the total to 7 KIA so far.
This has been a very costly deployment for the 48th Brigade so far, and it’s only a couple months into their 1 year tour.
Now, to less serious things.
Tyler Youngblood, proprietor of Projectsinmetal.com, noticed my post about the hammer I failed to make using his online plans. He took a moment to write a helpful comment, which I will repost here:
Hi Steve,
I’m sorry you’re having trouble with the soft faced hammer plans, but if it makes you feel any better, I scrapped the project twice before I got it right.
If I may make a few suggestions, maybe I can help. First, 304 stainless is far less forgiving than aluminum, which is what I made my hammer out of. It’s not as durable as stainless, but the hammer could be made fully functional by putting a pin into the head (the threaded head of my aluminum hammer comes loose with vigorous use). Locktite might also be an option. But I’m happy with the aluminum version for “light” hammering, which is what a soft faced hammer is good for anyway.
I didn’t turn the project between centers, but I had the benefit of a taper attachment, so that’s how I got the taper to work. If your compound slide has enough travel, you can definitely use that to put in your taper. Or you can buy/make a lathe dog for use with a proper face plate and do it that way. The only issue there is you mess with the alignment of the tailstock, which I try to avoid.
I’d suggest trying to use your compound to cut the taper. If you only have 2? of travel, change the taper to 2?. It would look different, but that’s fine, its your hammer.
Also, if you try to cut a taper using your compound, make sure to take light cuts. It sounds like you started cutting at the wide end of the taper, and by the time you got to the narrow end of the taper (3? later, up by the threads) you were cutting too much material. Instead, do it the other way. Start 1/4 inch back from the end of the taper and cut 1/4 inch in the direction of the threads, toward the radius. Your cut should gradually get a bit deeper, but since you’re only going 1/4? (and not 3?), the increased depth of cut shouldn’t be an issue. Once you have made that first pass, the rest of the cuts will be parallel to that first pass (thus no gradual increase to your depth of cut). After you’ve made that first pass of 1/4? or so, back your compound away from the part, then back along the axis of the taper you just cut. Your next pass should be 3/8? or so, then 1/2, …. all the way until your last pass takes a finish cut along the entire 3? taper.
It’s hard to explain. I really should make a video because it’s much easier if you see it done. As far as the radius goes, I used a tool with the proper radius to cut the taper, so when the taper was finished, the radius was already present. The radius on the end of the hammer was done with a file while the part was turning (make sure to hold the file backwards, with the tang facing away from you and cut from underneath the part, not on top – that way if the part rips the file out of your hand it will be pulled away from you). And of course, use a file with a handle whenever possible. No handle? Find an old golf ball, drill, and attach to the end of the tang. Tangs are sharp and dangerous.
You’ll need a mill to bore and tap the head of the hammer (where the handle attaches). You could do it on the lathe, but holding the part would require some significant workholding via the faceplate (I wouldn’t try it in a 4-jaw chuck, and a 3-jaw wouldn’t work at all). The threaded portions of the head where the faces attach are drilled on the lathe, but tapped after the larger hole is drilled, bored, and tapped on the mill.
For practice I single pointed the threads on the handle, but they can be cut with much less effort using a die. One of the scrapped handles was due to a mistake I made while cutting the threads.
Let me know if you’d be interested in me making a video of the process. I don’t really need another hammer, but I’d be happy to make a video if you think it would help (and if I can find the time).
Drop me a comment if you run into any other problems. I’d be happy to help in any way I can. I’m still learning too, so I remember how frustrating those first few projects were to master. But once you learn how to do all the steps in the hammer (turn down the dia, turn a taper, file a radius, knurl, single point (or tap/die) threads) you’ve got a very strong foundation and a good understanding of how the lathe works. That’s why the hammer, although difficult, is a great first project.
I’ve got another beginner project (a plumb bob) that uses hex stock, so if you’re interested in that (instead of the screw jack), let me know. Although the plumb bob is meant to be turned out of brass, not stainless. But stainless would work too.
Good luck!
Tyler Youngblood
ProjectsInMetal.com
Seattle, WA
That’s what I call service. I also got some good advice on the Chaski forum.
My biggest problem was trying to make the 3″ taper on the hammer handle. After I posted my whining, it occurred to me that I was probably cutting from the wrong end, and people have since confirmed this. When using a compound to cut a taper, start at the end where you have to remove the most metal. This way, the cuts are deepest as they begin, and they get shallower as you go. That will prevent problems with the cuts getting so deep the lathe throws up or whatever.
I learned a few other things. When trying to make a smooth transition from a straight piece into a taper which is thinner than the straight part, cut from the straight side. Say you have a taper that goes from half an inch to one inch, and you need a straight part one inch thick beyond the taper. You make the straight part too thick, and then you make the taper, and then you cut the straight part down, with cuts beginning at the end of the straight part which is farthest from the taper. The tool will cut off the excess metal from the straight part and then go into empty space as it hits the taper, leaving a smooth transition. At least, it worked that way for me.
I was told to use a file to make the small radii on the tool handle. That sure beats trying to grind a radius tool and then get it to make a perfect cut.
I blew the knurling. I am too lazy to get out my videos and see how it’s done, so I just winged it. No amount of skill can overcome true laziness. I know the knurls have to be perpendicular to the part, and the part has to be centered between the knurls. But I don’t know how to make them go into the same marks over and over as the part turns. I ended up with a surface that isn’t slippery, yet which would never be confused with real knurling.
I may dump this thing and use it for threading practice. It’s still a big piece of metal. There are lots of things I can make from it.
Here’s a photo of what I have. I put Dykem on it to help me line up the knurls.
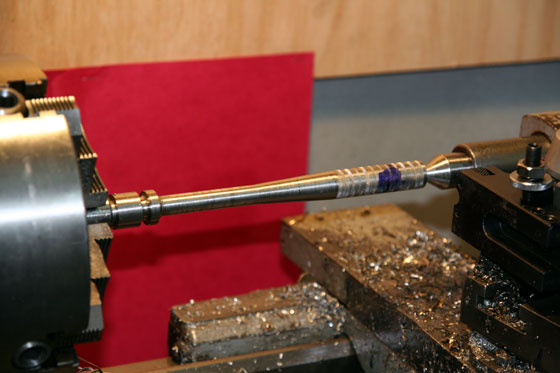
It’s not good, but I learned a great deal while working on it. And I ran the tool post into the work, and I also ran the carriage into the chuck. No pain, no gain. I just wish I had realized the carriage was blocking the chuck before I took the housing off the lathe to find out what was wrong with it.
Here is the latest news about the milling machine:
Hi Steve,
Sorry, Mark said that he did answer me, I think maybe there was an email problem.
It did ship last week, the driver should be calling soon, he will get the information for me later today, he was not in the office right now.
Thanks again!
Mark is the importer. Man, this is exciting.
I emailed Og for advice about turning parts to specified dimensions. He sent photos of his latest project.
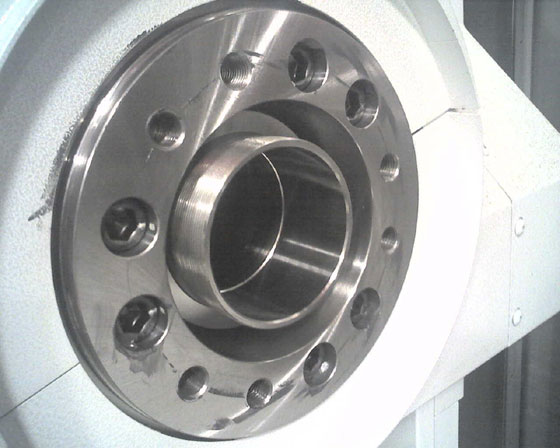
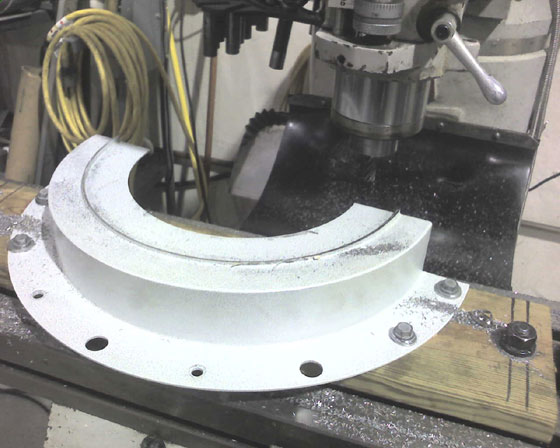
Yeah, I’m sure I’ll be doing this kind of stuff real soon. Notably, he used a crappy board for a base plate. I guess you never get too big for half-assed desperation jigs. I should start photographing the beauties I come up with.
Think I’ll take one of the bikes out and see if the wind blows the swarf out of my clothes. Sometimes I make splinters. Today I made several bona fide Slinkys.